Top Dyes for Soap and Detergent Industry
- Veeraco Colourants
- Oct 08, 2026
Introduction: Why Colour Selection Matters in Soap and Detergent Manufacturing
Colour is often one of the first things a customer notices about a soap or detergent. Before the product is touched, tested or smelled, its appearance has already created an expectation. In manufacturing, however, colour is not simply a visual decision. A shade that looks right in a laboratory sample can behave very differently after it meets surfactants, fragrances, builders, salts, alkalinity, heat or storage conditions.
So, what are the top dyes for soap and detergent industry applications?
There is no single dye that is universally suitable for every formulation. The most appropriate dye is the one that matches the chemistry of the product and remains stable throughout processing, packaging and storage. Solubility, pH compatibility, shade strength, chemical stability and interaction with other ingredients usually matter more than the name of the dye alone.
This is particularly important for industrial buyers and formulators. A colourant may provide strong colour at a low dosage, yet create staining, bleeding, shade variation or poor storage stability when introduced into the finished formulation. Conversely, a dye with excellent compatibility may require a different dosage or incorporation method to achieve the desired shade.
For this reason, selecting soap dyes and detergent dyes should be treated as part of formulation design rather than as a final decorative step.
What Are Dyes Used in the Soap and Detergent Industry?
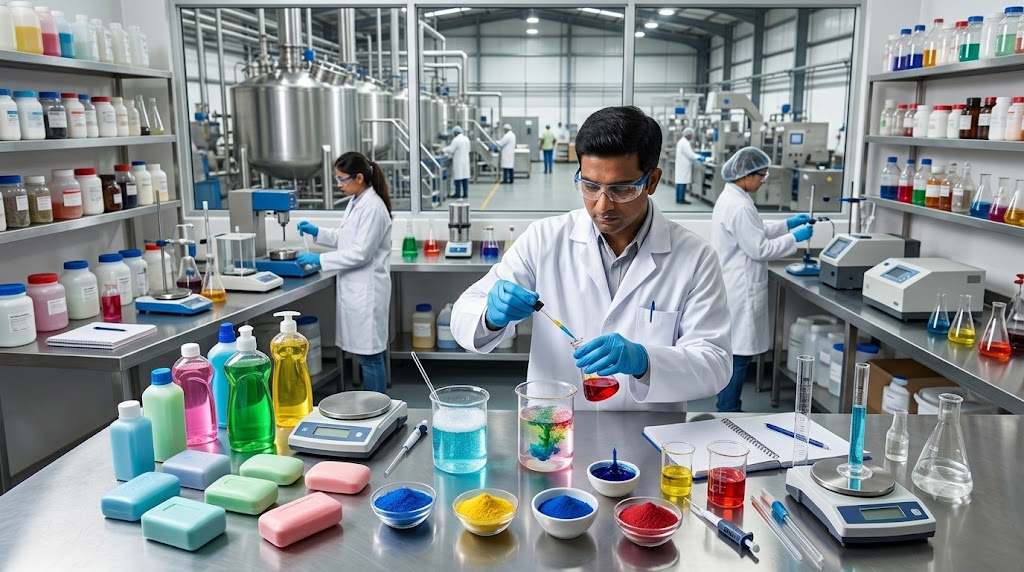
Dyes used in soap and detergent manufacturing are colourants selected to impart an even and recognisable shade to cleansing products. Depending on the formulation, they may be used in liquid products, solid soaps, detergent powders and other household or institutional cleaning formulations.
The key distinction is how the colourant behaves in the formulation. A water-soluble dye may be appropriate where rapid dissolution and uniform colour distribution are required. A liquid dye can simplify dosing and handling in some manufacturing systems, while a powder dye may suit applications where concentrated dry additions are preferred.
Not every commercial dye is automatically suitable for soap or detergent manufacture. Dyes developed for textile, paper or other industrial applications may have completely different performance requirements. Their suitability depends on factors such as solubility, ionic character, formulation pH, compatibility with surfactants and other ingredients, and the way the finished product will be stored and used.
The phrase “soap and detergent dyes” therefore describes an application requirement rather than one single chemical family. A formulator needs to start with the product chemistry and then select a colourant capable of working within that environment.
What Makes a Dye Suitable for Soap and Detergent Formulations?
Choosing suitable dyes for soap and detergents requires attention to how the dye behaves before, during and after production. A good colourant should not simply produce a strong shade. It should also remain predictable when exposed to the formulation's chemical environment.
Solubility and Dispersion
Solubility is one of the first technical parameters to evaluate. A dye that does not dissolve or disperse properly can produce streaks, specks, uneven colour or sedimentation.
In liquid soaps and detergents, water compatibility is often central to achieving homogeneous colour distribution. In powder detergents, the challenge can be different because the dye has to distribute consistently through a dry mixture without creating localised concentrations.
The practical point is simple: the colourant needs to match the physical form and incorporation method of the product. A formulation may require a dissolved dye solution, a liquid concentrate or a dry powder with suitable handling characteristics.
pH Compatibility
Soap and detergent products can operate across very different pH conditions. This matters because dye behaviour can change with acidity or alkalinity.
A colourant that performs well in one pH range may show shade shifts, reduced stability or altered solubility in another. Soap formulations in particular can present an alkaline environment, while detergent products vary substantially depending on whether they are liquid, powder or specialised cleaning formulations.
pH should therefore be treated as a selection parameter from the beginning. Laboratory testing of the actual formulation is more meaningful than selecting a dye based only on its nominal shade.
Chemical Stability
Soap and detergent formulations contain more than surfactants and water. Depending on the product, they may include builders, salts, fragrances, preservatives, solvents, enzymes or other functional ingredients.
The selected colourant should remain chemically stable in the presence of these components. Otherwise, the original shade may change over time or the dye may interact with other formulation ingredients.
A useful industry practice is to evaluate colour performance not only immediately after production but also after defined storage intervals. A sample that looks acceptable on day one does not necessarily represent its final performance.
Colour Strength and Shade Consistency
Industrial manufacturing depends on repeatability. Colour strength affects the amount of dye required, while shade consistency determines whether successive production batches look the same.
A highly concentrated colourant can reduce dosage requirements, but concentration alone does not guarantee good formulation performance. The dye must also develop the intended shade consistently at the selected addition level.
Colour measurement through controlled laboratory procedures can help formulators compare batches objectively rather than relying entirely on visual inspection.
Light and Storage Stability
A soap or detergent can spend weeks or months in warehouses, transport systems and retail environments before reaching the end user. Exposure to light, temperature changes, moisture and oxygen may affect colour stability.
Storage stability is therefore part of colourant selection. In applications where appearance is important, the chosen dye should be evaluated under realistic storage conditions rather than judged only in freshly prepared samples.
Compatibility With Surfactants and Other Ingredients
Surfactants are fundamental to detergent formulations, but they are not chemically identical across all products. Their interaction with dyes can influence solubility, shade development and overall formulation stability.
Other components can matter as well. Fragrance oils, salts, builders, solvents, preservatives and specialty additives may alter the environment in which the dye must function.
This is why a colourant should be tested in the final formulation or a close laboratory simulation. The actual product chemistry provides a much better indication of performance than water-based testing alone.
Top Types of Dyes for Soap and Detergent Industry
The most useful way to understand the top dyes for soap and detergent industry applications is to examine the categories by physical form and chemical behaviour rather than treating them as a universal ranking.
1. Water-Soluble Dyes
Water-soluble dyes are particularly relevant where colour needs to dissolve readily in an aqueous formulation. They can support uniform colour distribution when the formulation and processing conditions are compatible.
For liquid soaps and detergents, water solubility can simplify incorporation and reduce the risk of undissolved colourant particles. However, high solubility by itself is not enough. The dye must also remain stable at the formulation's pH and in the presence of the other ingredients.
Water-soluble dyes can also be useful where very small amounts of colourant are needed. Because dye strength varies considerably by product, dosage should be determined through controlled trials rather than assumed from the appearance of a concentrated solution.
2. Liquid Dyes
Liquid dyes are concentrates designed to provide a convenient route for dosing and incorporation. In automated or semi-automated production environments, this can make colour addition easier to control.
The main technical questions are whether the liquid system remains homogeneous during storage, whether it can be accurately metered and whether the dye performs consistently after introduction into the final formulation.
Liquid dyes can therefore be attractive from a process-control perspective, but the appropriate product still depends on the chemistry of the soap or detergent being manufactured.
3. Powder Dyes
Powder dyes remain relevant where the manufacturing process is designed around dry raw materials. They can be used in systems such as powdered detergents when the colourant can be distributed evenly through the formulation.
The challenge is uniformity. If a highly concentrated powder is added without adequate mixing, localised colour pockets can form. This may cause visible shade variation from one part of a batch to another.
For dry detergent systems, particle characteristics, addition sequence and mixing efficiency can be just as important as the colourant itself.
4. Fluorescent Dyes and Brighteners
Fluorescent colourants and optical brighteners require careful distinction because optical brighteners are not simply conventional colouring dyes. Their purpose is associated with optical effects such as increasing perceived whiteness or brightness rather than creating a conventional visible shade.
Optical brighteners work by absorbing ultraviolet radiation and re-emitting energy in the visible range, which can make materials appear brighter. The actual role and suitability depend heavily on the substrate and formulation.
For detergents, brightening technologies are more closely associated with laundry performance and whiteness perception than with colouring a product blue, green, pink or another visible shade. They should therefore be evaluated against the formulation's intended function rather than grouped with ordinary soap dyes without qualification.
5. Acid Dyes
Acid dyes are generally known for their application on substrates such as wool, silk and nylon, with performance governed by their anionic, water-soluble chemistry.
That does not make acid dyes a universal solution for soap and detergent colouring. Their use in cleaning formulations requires specific compatibility testing. In an industrial context, the question should not be whether a dye belongs to a familiar dye class, but whether its chemistry is appropriate for the finished product.
6. Basic Dyes
Basic dyes are cationic colourants and are widely associated with substrates such as acrylic fibres and paper because of their positive charge.
For soap and detergent applications, the same principle applies: the dye should only be selected after evaluating formulation chemistry, compatibility and intended use. A basic or cationic dye should not be treated as automatically suitable simply because it provides a brilliant shade.
7. Other Synthetic Dyes Used in Cleaning Formulations
Some cleaning product applications use specialised synthetic colourants selected for particular formulation requirements. These may be designed around parameters such as low staining, controlled solubility, high colour intensity or improved stability.
The choice becomes more specialised as the formulation becomes more complex. Household, industrial and institutional cleaning products may have very different chemical environments, which means a colourant suitable for one application may not perform the same way in another.
For example, Veeraco Colourants currently identifies certain solvent dyes as specifically selected for detergent applications in household, industrial and institutional cleaning products, with emphasis on stability and minimal staining behaviour. Actual suitability still needs to be established for the specific formulation.
Best Dyes for Different Soap Applications
Different soap products create different technical demands, so the best dye for one soap category may not be appropriate for another.
Dyes for Toilet and Bathing Soaps
Toilet and bathing soaps typically require attractive, uniform colour that remains stable throughout manufacturing and storage. The colourant should not create visible spotting, excessive bleeding or unwanted transfer to packaging and adjacent materials.
The formulation's base, fragrance system, pH, moisture and processing temperature should all be considered during dye selection. Transparent and opaque soap bases can also reveal colour differences differently, making laboratory testing important.
Dyes for Liquid Soaps and Hand Wash
Liquid soaps and hand washes generally place greater emphasis on water solubility and homogeneous distribution because the finished system is fluid.
A suitable dye should remain evenly distributed without producing sedimentation or visible separation. The formulator must also consider the effect of surfactants, preservatives, fragrances and other ingredients on shade stability.
In production environments, liquid colour concentrates may offer practical dosing advantages when the manufacturing system supports controlled liquid addition.
Dyes for Transparent and Glycerine Soaps
Transparent soaps are less forgiving of formulation defects because suspended particles, haze or uneven colour are easily visible through the product.
The colourant therefore needs to dissolve or distribute in a way that preserves the visual characteristics of the soap base. A colourant that works acceptably in an opaque formulation may produce an entirely different visual result in a transparent base.
This makes compatibility and clarity testing particularly important when selecting dyes for transparent or glycerine soaps.
Dyes for Industrial and Specialty Soaps
Industrial and specialty soaps may have functional formulations designed for specific cleaning, processing or technical applications. Their colour requirements can be practical rather than purely decorative.
For example, colour may help users distinguish product grades, concentrations or intended uses. In such cases, shade consistency across production batches becomes especially important because the colour can function as part of product identification.
Best Dyes for Different Detergent Applications
Detergent formulations can differ significantly in physical form and chemistry. Consequently, detergent dyes should be selected with the final product and production process in mind.
Dyes for Liquid Detergents
Liquid detergents typically require excellent dissolution or dispersion and reliable stability in a surfactant-rich environment.
The colourant should remain homogeneous throughout storage and should not create excessive staining or unwanted interaction with the formulation. A concentrated liquid dye can be considered where precise dosing is important, while water-soluble systems may be suitable when the formulation chemistry allows easy dissolution.
Dyes for Powder Detergents
Powder detergents create a different challenge because the colourant must be distributed through a dry formulation.
Uniform mixing becomes critical. A strongly coloured material added in a concentrated form may create uneven colour distribution if the powder's particle characteristics and mixing process are not properly matched.
For this reason, dye selection and manufacturing process design should be considered together. Addition sequence, premixing and final blending can influence the visible result as much as the dye itself.
Dyes for Laundry Detergents
Laundry detergents require especially careful consideration because the finished product comes into direct contact with fabrics.
The desired product colour and the behaviour of the dye during use are separate considerations. A detergent colourant should not create unacceptable staining or transfer under normal use conditions.
The detergent's surfactant system, alkalinity and other ingredients should therefore be included in performance testing. Where optical brighteners are used, they should also be considered separately from conventional product colourants because they perform a different optical function.
Dyes for Dishwashing and Household Cleaning Products
Dishwashing liquids and household cleaners can contain complex combinations of surfactants, solvents, preservatives, fragrances and other additives.
Here, colourants need to provide a stable appearance without negatively affecting the formulation. The product's packaging, exposure to light and expected shelf period may also influence the required level of colour stability.
A formulation that remains bright and uniform during manufacturing but fades during warehouse storage does not meet the same performance standard as one that remains stable throughout its intended lifecycle.
How to Choose the Right Dye for Soap and Detergent Manufacturing
The most reliable approach is to select the dye against the formulation rather than selecting the formulation around a preferred colourant.
Consider the Formulation pH
Start by identifying the actual pH range of the finished product and the expected variation during manufacturing and storage.
The dye should remain stable within that environment. Testing only at neutral pH can produce misleading conclusions when the final product is strongly acidic or alkaline.
Check Dye Solubility
Determine whether the dye should dissolve completely, disperse uniformly or be incorporated in another controlled form.
Solubility should be evaluated in the actual formulation environment because salts, surfactants and other ingredients may affect the behaviour observed in water alone.
Evaluate Chemical Compatibility
Review the interaction between the dye and the formulation's principal ingredients. Particular attention should be given to surfactants, builders, salts, fragrances, preservatives and other reactive components.
Compatibility testing can identify precipitation, shade shifts, staining or instability before the colourant moves into full-scale production.
Assess Colour Strength and Dosage
Determine the concentration required to reach the target shade while maintaining process consistency.
The objective is not simply to use as little dye as possible. It is to achieve the required shade reproducibly with a controlled dosage that remains practical for manufacturing.
Test Colour Stability
Stability should be evaluated over time, not only immediately after production.
Samples can be observed under controlled storage conditions for changes in shade, clarity, sedimentation or separation. Where relevant, exposure to light and temperature variation should also be included.
Consider Processing Conditions and Storage
Processing temperature, mixing time, order of addition and storage conditions can all influence colour performance.
A dye that performs correctly under laboratory mixing may behave differently in a large production vessel. Scale-up trials are therefore valuable before finalising the commercial formulation.
Common Problems When Using the Wrong Dye
Colour-related problems in soap and detergent production are rarely limited to aesthetics. They can also create manufacturing inconsistency, product complaints and unnecessary rework.
Colour Fading
Fading may result from exposure to light, heat, oxygen or chemically incompatible ingredients. If the formulation environment is harsher than the dye's stability range, the original colour may not remain intact.
Bleeding and Migration
Bleeding occurs when colourant moves from the product into another phase or material. In cleaning products, excessive staining behaviour can be particularly undesirable.
The risk depends on dye chemistry, concentration, formulation and the conditions under which the product is stored or used.
Uneven Colour Distribution
Uneven mixing can create streaks, spots or patches. This is especially relevant to concentrated liquid colours and highly coloured powders.
The solution is not necessarily a different dye. It may require better premixing, a different addition method or improved process control.
Shade Variation
Small differences in concentration, raw material composition, pH or processing can result in visible shade variation.
For manufacturers supplying repeat orders, this can become a major quality issue. Consistent raw materials and controlled colour measurement can reduce the problem.
Poor Stability During Storage
Some colourants perform well at the point of manufacture but become unstable during extended storage.
This is why shelf-life testing should be treated as part of colourant approval rather than as a separate quality exercise.
Interaction With Other Formulation Ingredients
A dye may interact with fragrances, surfactants, salts or other additives in unexpected ways. Such interactions can change colour strength, clarity, dissolution or overall appearance.
The more complex the formulation, the more important it becomes to evaluate the complete system rather than one ingredient at a time.
Soap and Detergent Dye Selection: A Practical Comparison
| Requirement | Soap Applications | Detergent Applications |
|---|---|---|
| Solubility | Important | Important |
| pH stability | Critical | Critical |
| Colour strength | Important | Important |
| Chemical compatibility | Critical | Critical |
| Storage stability | Important | Important |
| Shade consistency | Critical | Critical |
The comparison shows why a single “best dye” is difficult to define. Soap and detergent manufacturers may share broad requirements, but the exact formulation determines which properties receive the greatest weight.
For one product, rapid water dissolution may be the key requirement. For another, low staining may matter more. Powder detergents can place stronger emphasis on dry mixing and distribution, while liquid systems may focus on dissolution and long-term homogeneity.
The technically correct choice is therefore the one that satisfies the complete set of requirements for the specific formulation.
Conclusion: Selecting Dyes Based on Formulation and Performance
The search for the top dyes for soap and detergent industry applications should begin with a change in perspective. The strongest shade is not necessarily the most suitable, and the most concentrated colourant is not necessarily the most economical after manufacturing variables are considered.
The real objective is controlled colour performance.
That means matching the dye to the product's pH, physical form, surfactant system, processing conditions and storage environment. Water-soluble dyes, liquid dyes, powder dyes and specialised colourants can each have a role, but their value depends on how well their chemistry fits the formulation.
For industrial buyers and formulators, supplier evaluation should also extend beyond shade samples. Technical documentation, batch consistency, quality-control procedures, sample testing and the ability to support application-specific requirements can all influence sourcing decisions. Veeraco Colourants describes its operations around dyes, pigments and specialty colourants, with manufacturing and sourcing partnerships, technical shade-matching capability and quality-control processes for industrial and export requirements.
In the end, colour is only successful when it remains predictable after the product leaves the laboratory. That is where dye selection becomes less about finding a “top” product and more about understanding the chemistry of the formulation, the realities of manufacturing and the performance expected throughout the product's life.
For application-specific dye evaluation, Veeraco Colourants provides technical information and sourcing support for industrial colourant requirements.
Frequently Asked Questions
Soap manufacturers may use application-specific synthetic colourants, including water-soluble and liquid or powder forms, depending on the soap base and manufacturing process. Suitability depends on pH, solubility, stability and compatibility with the complete formulation.
Dyes that dissolve or disperse consistently in the detergent base are generally considered first, but the final choice depends on surfactants, pH, salts, fragrances and other ingredients. Laboratory testing in the actual detergent formulation is important.
Sometimes, but not automatically. Soap and detergent formulations can differ significantly in pH, surfactant chemistry and other ingredients. A dye that performs well in one product needs to be tested before being transferred to another application.
Water-soluble dyes can be suitable for detergent formulations where their chemistry is compatible with the product. Solubility alone does not determine suitability. Stability, staining behaviour, shade consistency and interaction with formulation ingredients must also be considered.
The selection should consider the dye's compatibility with the dry detergent system, colour strength, particle characteristics, storage stability and mixing method. Uniform distribution through the powder is particularly important.
Soap dye stability can be influenced by pH, formulation ingredients, processing temperature, light exposure, storage conditions and the chemical stability of the dye itself.
There is no universal dosage. The required amount depends on dye strength, target shade, formulation composition and the physical form of the colourant. Dosage should be established through controlled laboratory trials and then confirmed during production-scale testing.
Start with a colourant that is compatible with the formulation and evaluate staining behaviour at the intended dosage. Proper dissolution, dispersion and mixing are equally important because excessive local concentration can increase the risk of uneven colour behaviour.